For a frozen seafood processor, losing one forklift during a dispatch window can mean delayed pallets, a waiting truck and additional handling outside the required temperature zone. Yet the cause is not always a mechanical failure. It may be a battery that cannot complete the duty cycle, water that freezes after repeated doorway crossings, or a truck that needs too much room to turn in a packed cold store.
Selecting a Forklift for Cold Storage Thailand project is therefore a workflow decision before it is a purchase decision. The right truck must handle the load, fit the warehouse and operate within the actual temperature limits of its battery, hydraulics and electrical system.
This guide is written for Thai cold-chain operators, including seafood processors, fruit exporters, frozen-food distributors and third-party logistics (3PL) warehouses. It explains what to measure, where specifications can be misleading and how to compare practical equipment options without assuming that every electric forklift is freezer-rated.
I. Start With the Thai Warehouse, Not the Forklift Catalogue
A frozen seafood warehouse and a chilled fruit warehouse have different problems
Consider a seafood operation in Samut Sakhon handling frozen cartons at approximately -18°C, subject to the product's actual storage specification. Pallets may move from a freezer to a loading dock several times per hour. The difficult part is often the transition: a cold truck meets warm, humid air, then returns to a freezing room before moisture has dried.
A fruit distribution warehouse in Chanthaburi may operate mostly above freezing, with temperatures tailored to the fruit variety. Here, pallet turnover, limited aisle space, product damage and charging between shifts may matter more than extreme-low-temperature capability.
A multi-temperature 3PL facility near Bangkok has a third challenge: different customer products may require separate chilled and frozen zones, while dispatch schedules change throughout the day. One forklift may not be the most efficient answer for every zone.
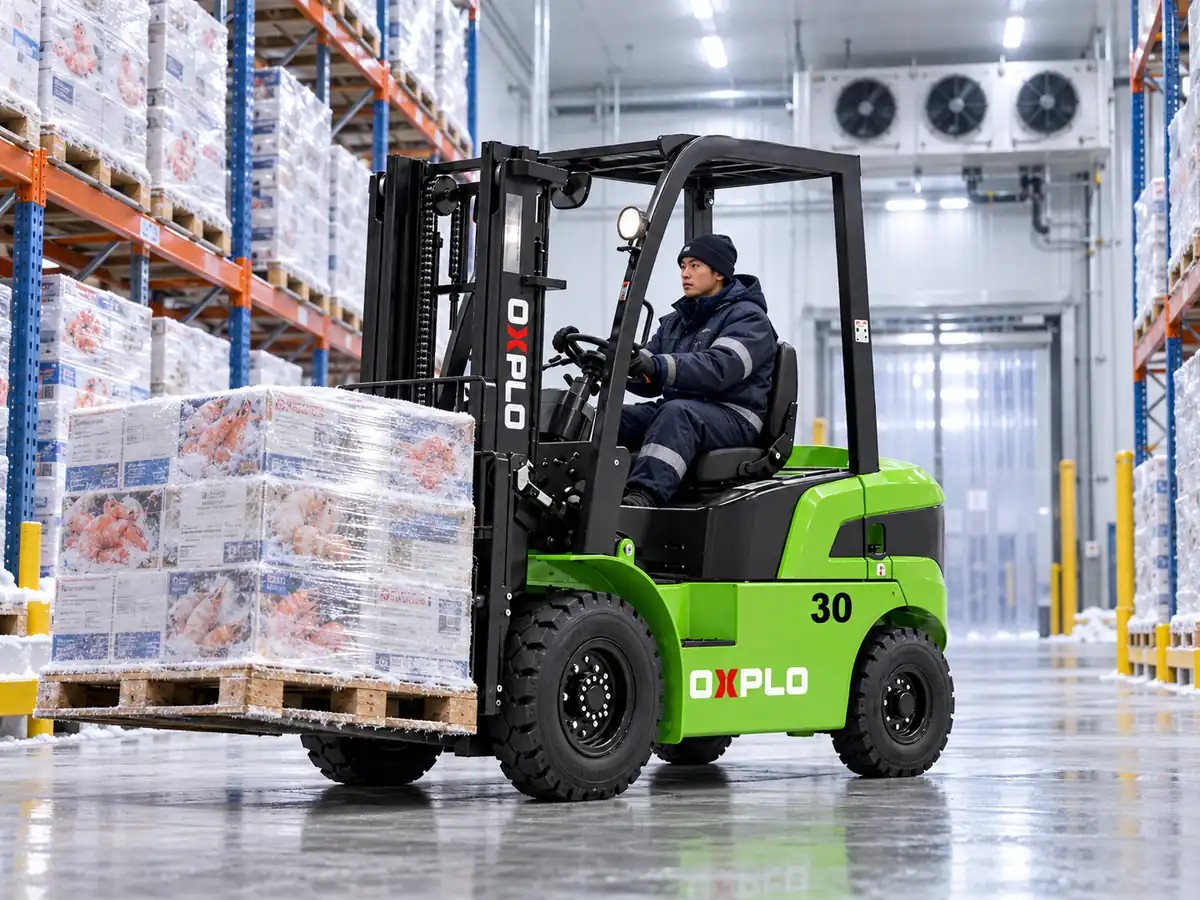 Figure 1. An OXPLO-style electric forklift handling packaged frozen seafood. Illustrative scene; cold-store approval must be confirmed for the actual machine.
The phrase “2.5-ton electric forklift for cold storage” is not a complete specification. Temperature, time spent inside the room, door-crossing frequency, pallet size and working hours can change the recommendation even when the rated load is identical.
Define the actual operating zones
Record the lowest and normal temperatures of each area, plus how long the forklift stays there. Do not confuse chilled storage with continuous freezer duty. A machine that works in a +4°C food warehouse is not automatically approved for eight hours at -20°C.
Just as important, identify where the forklift waits between tasks and where it charges. These locations affect both battery temperature and condensation exposure.
II. Battery Selection: Can the Truck Finish the Real Shift?
Nominal capacity is not guaranteed runtime
Lithium-ion and lead-acid batteries both lose available performance as temperatures fall, although their behavior and management systems differ. In cold storage, what matters is the energy actually available for travel and lifting after temperature effects, operating reserves and charging restrictions.
The first request to a supplier should not be “How many hours on one charge?” without context. Instead, provide the average pallet weight, lift height, travel distance, number of lifts, ambient and cold-room temperatures, and the time available for charging.
For technical background, consult Crown Equipment's cold-storage battery guidance. It explains why low temperatures change battery behavior and why a battery-handling strategy matters in cold facilities.
A simple, transparent battery calculation
Take a hypothetical electric forklift with a 76.8V / 280Ah battery. Its nominal stored energy is:
Nominal energy (kWh) = 76.8 × 280 ÷ 1,000 = 21.5 kWh
Suppose the procurement team applies a planning usable fraction of 70% to account for reserve and site-specific allowances, then assumes 3.0 kW average operating demand. The illustrative estimate becomes:
Estimated runtime = (21.5 × 0.70) ÷ 3.0 ≈ 5.0 hours
These are assumptions for an example, not verified cold-room performance figures for any particular truck. Actual energy use depends on the lift cycle, driving pattern, battery condition, thermal management and temperatures. A different duty cycle could produce a very different result.
For an eight-hour dispatch shift, that five-hour planning estimate signals a question: can the truck charge during a break, must the route be reorganized, or is additional equipment required? Do the calculation before specifying a battery or promising a shift length.
Check three temperature limits separately
· Discharge: lowest approved battery-cell and truck operating temperature under load.
· Charging: permitted cell temperature for charging and whether an approved battery-heating system is required.
· Parking/storage: temperatures and durations allowed when the forklift is idle.
A battery permitted to discharge in a freezer is not necessarily permitted to charge there. Some specialized cold-store lithium systems have heating arrangements, but their capabilities must not be inferred from the word “lithium” on a product page.
Figure 2. Pre-shift inspection and charging-system checks. Charging conditions must follow the approved battery and charger specifications.
Where lithium-ion can help—and where it does not
For suitable operating conditions, lithium-ion can simplify routine maintenance because there is no flooded lead-acid battery watering. Battery-management monitoring can also support diagnosis and operating discipline. Opportunity charging may be practical when the battery, charger and charging environment meet their approved limits.
None of these advantages removes the need to check the whole forklift. Hydraulic fluid, seals, electrical connections, brakes and operating procedures must also be suitable for the planned temperature exposure.
III. Condensation: The Doorway Problem Most Buyers Underestimate
What happens when a cold forklift enters warm Thai air?
A freezer truck leaves a -20°C room. Its cold surfaces meet warmer air at the loading dock. If those surfaces are below the air's dew point, water condenses. The truck then returns to the freezer; water left on exposed parts can freeze.
Repeated cycles can contribute to ice around components, impaired visibility, electrical problems and additional inspection time. Condensation is particularly difficult because the problem may originate at the warm dock, even though the symptom appears inside the freezer.
The discussion in Toyota Material Handling's guidance on cold-room condensation makes the same operational point: temperature transitions and drying procedures are central to equipment reliability.
Figure 3. The transition between a freezer and a loading area introduces condensation risk. Illustrative warehouse scene.
Fix the flow before buying another machine
Map every forklift trip that crosses a cold-room boundary. Ask whether the same truck must both retrieve pallets from a freezer and load ambient-side trailers. A two-zone handover can be worth evaluating:
· A cold-zone truck stays primarily in the approved low-temperature zone.
· A dock-zone truck moves pallets through staging and truck loading.
· A controlled handover point minimizes unnecessary truck temperature transitions.
This is not a universal recommendation to buy two forklifts. Two-zone handling adds transfer time, space requirements and potentially another operator. Compare those costs with the present crossing frequency, ice incidents and avoidable stoppages. For a small facility, one properly approved machine and a disciplined route may be more economical.
The freezer doorway is part of the equipment system
Inspect door seals, opening duration, staging humidity, drainage and floor ice near the threshold. Fast-closing insulated doors can reduce air exchange, but door detection, traffic signals and pedestrian separation must remain safe. A door improvement may reduce the conditions causing repeated moisture exposure without changing the forklift.
Ask the equipment manufacturer for approved drying, parking and re-entry procedures. Do not impose a generic drying time across different trucks; the operating limits may differ by model and configuration.
IV. Floors, Tires and Aisles: Why a Bigger Truck Can Handle Fewer Pallets
Wet concrete and ice affect safe operation
A cold-room aisle may look smooth, but the loading dock and doorway can be wet or icy. Traction and braking must be checked on the actual surfaces. Tire compound and tread must be approved for the operating environment; no tire specification makes uncontrolled ice safe.
Review the dock ramp, joints, potholes, floor drainage and cleaning practices. If operators avoid a slippery doorway or take extra correction movements in a tight aisle, the throughput penalty may be larger than expected.
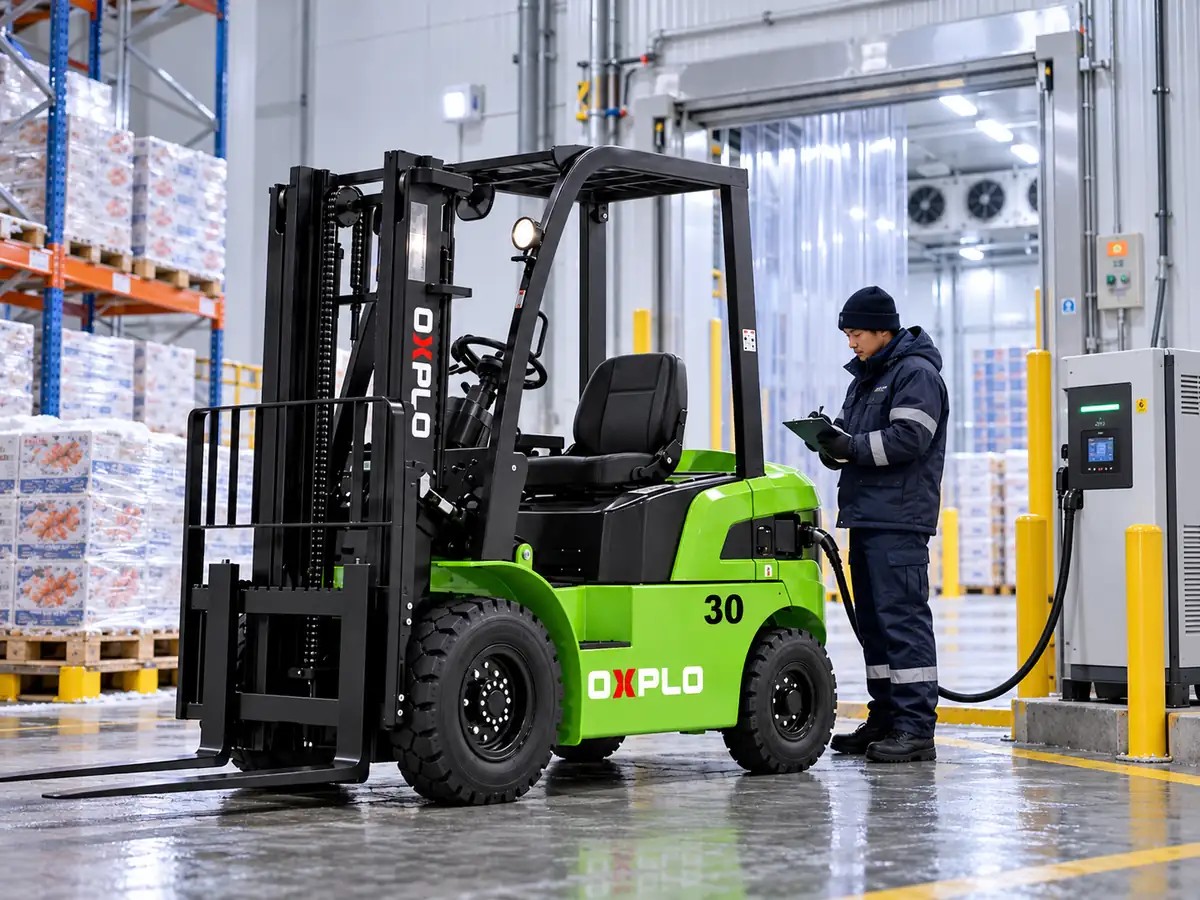
Figure 4. Moisture on cold-storage floors can affect traction and braking. Evaluate the actual operating surfaces.
Compare load center and residual capacity, not just tonnage
The 2-ton or 3-ton figure on a nameplate normally applies at a specified load center and configuration. A long pallet, high stacking position or added attachment can reduce the available lifting capacity. Obtain the residual-capacity information for the intended mast and attachment.
Also check the floor structure. A freezer floor can incorporate insulation and a slab with specified wheel/axle loading limits. Rated lifting capacity is not the same as the pressure imposed by a loaded truck. The floor engineer should assess the selected machine's actual wheel and axle loads.
Aisle width is a cost variable
Do not compare only the truck's overall width with the doorway. Confirm right-angle stacking space, turning radius, pallet geometry, fork length, mast height, overhead clearance and pedestrian separation. Every unnecessary positioning movement consumes battery and time.
A larger counterbalance forklift may be appropriate for heavy pallets, but a more compact capacity class can be a better fit where most loads are lighter and storage aisles are tight. This trade-off becomes especially important in a temperature-controlled building where floor area is expensive to construct and refrigerate.
V. Calculate Total Cost of Ownership Around Pallet Movements
Count productive time, not simply machine hours
A useful efficiency measure is productive pallet movements per hour, supported by the battery energy consumed per 100 pallet movements. These connect forklift selection with dispatch capacity rather than brochure specifications.
Consider an illustrative warehouse making 30 unnecessary warm/cold transitions each day. If changing the route saves an average of two nonproductive minutes per crossing:
Time recovered = 30 × 2 minutes × 26 days ÷ 60 = 26 hours/month
That is not a claimed customer result. Real savings may be smaller after accounting for handover work or increased fleet cost. Nevertheless, the calculation shows why route design and door operations deserve attention alongside battery size.
Include indirect costs in the comparison
Calculate the total relevant cost over a consistent period and divide by productive pallet movements. This can reveal why a lower-cost forklift is not always the lower-cost operation—and why a special low-temperature package is not justified for every chilled warehouse.
VI. A Seven-Point Buying Checklist for Thailand Cold-Chain Operators
Give suppliers measurable operating conditions
Before asking for a quotation, assemble this information in one sheet:
1. Temperature map: minimum and normal temperatures for each room and dock.
2. Exposure profile: minutes per trip in each zone and doorway crossings per day.
3. Loads: heaviest pallet, pallet dimensions, load center and required lift height.
4. Layout: door widths, right-angle stacking aisle, ramp and overhead clearances.
5. Shift plan: operating hours, peak movements and realistic charging windows.
6. Environment: wet or icy floor locations, drainage and floor loading limits.
7. Support: local maintenance access, spare parts, warranty boundaries and operator training.
Do not accept “suitable for cold storage” as the only written confirmation. Ask for model-specific minimum operating temperature, duration limits, battery discharge and charge limits, hydraulic fluid, relevant seals and moisture-management procedures.
Use a three-scenario decision rule
Trial the actual job before expanding the fleet
If the application is demanding, pilot the selected configuration on representative pallets, aisle routes and temperature transitions. Record battery warnings, consumed kWh, pallet movements, moisture incidents and stopping/turning performance on safe, approved surfaces.
The best result is not merely “the truck moved the pallet.” It is documented evidence that the configuration can do the job over the planned duty cycle without creating new operational bottlenecks.
VII. Where OXPLO Electric Forklifts Fit the Buying Decision
Once the warehouse requirements are documented, it becomes possible to compare machine dimensions, capacity and support arrangements. OXPLO's forklift range includes electric counterbalance models for indoor material handling, food and beverage storage and logistics work. OXPLO's published standard specifications do not, on their own, establish continuous deep-freeze approval. Buyers should confirm any required cold-room configuration in writing.
OXPLO CPD20: When aisle space and standard pallet loads matter
The OXPLO CPD20 electric forklift is rated at 2,000 kg with a 500 mm load center. Its published width is 1,164 mm, minimum outer turning radius 2,190 mm and minimum right-angle stacking aisle width 2,230 mm. The listed lithium battery is 76.8V / 280Ah.
For a chilled distribution warehouse with suitable operating temperatures and loads within the verified capacity envelope, OXPLO CPD20 may be worth assessing where maneuverability matters. OXPLO's electric drive avoids diesel tailpipe emissions at the point of use, while its BMS monitors battery conditions. Neither feature alone proves that the truck is suitable for a freezing room.
OXPLO CPD25: A middle capacity class for mixed pallets
The OXPLO CPD25 electric forklift is rated for 2,500 kg at a 500 mm load center. Its published width remains 1,164 mm, while its minimum outer turning radius is 2,240 mm and listed minimum right-angle stacking aisle width is 2,280 mm. The standard published battery is also 76.8V / 280Ah lithium.
For operators whose normal load requires more than the 2-ton class, OXPLO CPD25 provides an intermediate option to evaluate before automatically moving up to a larger truck. The decision still depends on residual capacity, floor strength and temperature approval.
OXPLO CPD30: Higher rated load, greater space requirement
The OXPLO CPD30 electric forklift is rated at 3,000 kg at a 500 mm load center. Its published overall width is 1,225 mm and minimum outer turning radius is 2,515 mm, with a minimum right-angle stacking aisle width of 2,545 mm. Its listed lithium battery is 76.8V / 280Ah.
OXPLO CPD30 may be relevant where heavier pallet loads justify the capacity and the warehouse can accommodate the truck's dimensions and wheel loads. It is not automatically more productive in narrower aisles, nor automatically cold-store rated.
Compare OXPLO models against a real warehouse requirement
Specifications reflect the currently published standard model pages; actual configuration, pallet dimensions, attachments, clearance and residual capacity must be verified. None of these figures constitutes freezer approval.
What OXPLO can address—and what must be confirmed
For approved indoor applications, OXPLO's published product features offer a useful set of practical advantages: an electric drivetrain with no tailpipe exhaust, lithium battery/BMS monitoring, different lifting capacities and model dimensions to fit varying warehouse layouts. These address common procurement questions about indoor operation, load handling, routine maintenance and aisle efficiency.
For a cold-storage project, OXPLO should then check the additional questions the standard brochure cannot settle: minimum permitted truck temperature, lithium charge/discharge limits, required hydraulic oil and seals, tire choices, moisture procedures and any specially approved configuration.
The OXPLO warehouse handling solution explains the company's general pallet-handling focus. The OXPLO service and support page describes pre-sales consultation, parts supply and after-sales arrangements. The OXPLO Thailand operations page provides context on the regional business presence. For any specific site, confirm parts, response arrangements and warranty coverage in the written offer rather than assuming a universal service level.
Figure 5. An OXPLO-style electric forklift moving palletized goods in a cold-chain loading area. Illustrative scene.
OXPLO can be part of a technically disciplined purchasing process. The goal is to match an OXPLO model and approved configuration to an actual duty cycle—not to claim that every OXPLO electric forklift is a freezer-specialist machine.
VIII. Frequently Asked Questions
Can a standard electric forklift run continuously at -18°C?
Not without explicit manufacturer approval for that temperature and duration. Cold-operation capability must cover the complete truck, not just the traction battery. Ask OXPLO or any other supplier for the exact approved configuration and limitations.
Is lithium-ion always better than lead-acid in a Thai cold store?
Not always. Lithium-ion can simplify routine servicing and support certain charging strategies, but temperature limits, thermal management and lifetime cost matter. The right choice depends on the actual shift and charging conditions.
Why does ice form on the forklift after it leaves the freezer?
Cold components can collect condensation from warmer humid air. If moisture remains when the forklift goes back into a freezing environment, it can form ice. Doorway management and an approved drying/re-entry process are essential.
Should a seafood warehouse buy a 3-ton forklift instead of a 2-ton unit?
Only if the pallets, load center, lift height and attachments require the capacity. A larger truck can demand more turning space and place higher loads on the floor. Compare the relevant OXPLO models against the actual warehouse plan.
Can I charge a lithium forklift in the freezer?
Only if the complete battery and charging system are specifically approved for that temperature and installation. A published lithium battery rating does not establish low-temperature charging permission.
What information should I send when asking OXPLO for a quotation?
Send the minimum temperature, pallet weight and size, load center, lift height, aisle and door dimensions, floor conditions, operating hours, crossings between zones and charging opportunities. OXPLO can then discuss suitable standard models and identify configuration points requiring technical confirmation.
IX. Conclusion: Buy for the Cold-Chain Workflow, Not a Single Specification
A Forklift for Cold Storage Thailand operation must do more than lift the right weight. It must fit the aisles, complete the work cycle, remain within approved temperature limits and avoid avoidable moisture-related interruptions. For frozen seafood facilities, the freezer-to-dock transition may be the defining risk. For chilled produce warehouses, aisle fit and loading efficiency may be more important.
The most defensible buying process is to measure the warehouse first, estimate the duty cycle, verify temperature compatibility and only then compare models. OXPLO offers several electric capacity classes and Thailand-based sales and support information that can inform that comparison; low-temperature suitability must still be confirmed for the specific equipment offered.
To assess an OXPLO forklift for your cold chain, send your temperature, load, aisle and shift requirements through the OXPLO contact page.
สอบถามตอนนี้